The label may say bamboo, but the printer sees rayon. Almost every soft bamboo tee on the market is bamboo viscose, a cellulosic fiber regenerated from bamboo pulp. That single fact drives every decoration decision that follows, because viscose is more heat-sensitive than cotton and far more delicate than polyester. Choose a method that ignores this and you get scorched sheen, a stiff hand on a fabric people buy for its softness, or a print that cracks after a dozen washes. This guide compares the four decoration methods you will actually be quoted on, with the temperature and durability details that separate a good result from a reprint.
Start with the fiber, not the ink
Bamboo viscose jersey typically lands between 140 and 180 grams per square meter, lighter and drapier than a standard 180 gsm cotton tee. It behaves like a semi-synthetic cellulose: it takes water-based color well, but it softens and glazes under heat that cotton would shrug off. Decorators repeatedly warn that viscose can develop a permanent shiny or scorched patch at high press temperatures, and that it shrinks if it meets hot water or a hot dryer. Two consequences follow. First, whatever method you pick has to work at the lowest reliable temperature. Second, the finished garment needs a cold-wash, low-heat care instruction, and it is worth printing that on the label so your customer does not undo your work in the laundry.
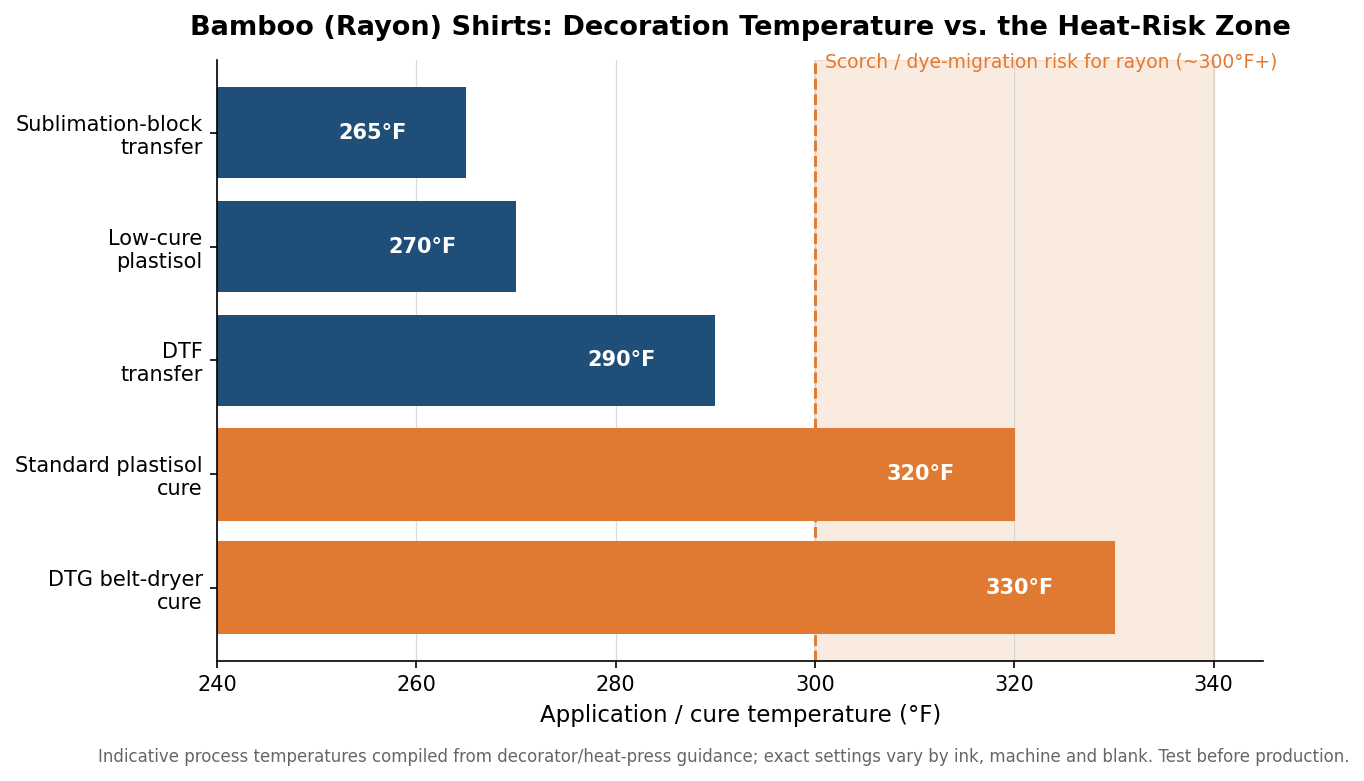
The chart below places the common decoration processes against the zone where rayon starts to get into trouble. Anything pushing past roughly 300°F is where dye migration and surface glazing become real risks on a viscose blank.
Screen printing: the most durable print, if you control the cure
For a simple one- to three-color logo in volume, screen printing still gives the toughest, longest-lasting result. A properly cured plastisol print routinely survives 50 or more wash cycles with minimal fade. The catch is the cure: standard plastisol needs its whole ink film to reach about 320°F to fully cross-link, and that is right in the rayon danger band. The fix is a low-cure plastisol formulated to fuse near 270°F, which keeps the fabric well under its scorch threshold while still curing hard. Ask your decorator specifically whether they are running a low-cure ink and verifying it with a temperature gun or test strip rather than eyeballing the belt.
Watch dye migration on colored blanks. Deep reds, maroons and some blues carry disperse-type dyes that can reactivate and bleed up into a light print once the ink film climbs above roughly 300°F, leaving a white logo looking pink days later. On darker bamboo garments, a low-bleed or blocker-based ink and the lowest workable cure temperature are the practical defenses. Also be realistic about water-based and discharge inks: discharge relies on bleaching the garment dye and is engineered around reactive-dyed cotton, so it is unreliable on viscose and often will not discharge cleanly. Standard water-based inks can work but need careful curing to avoid under-cure on this fiber.
DTG and DTF: full color and short runs without a screen
Direct-to-garment printing suits bamboo well on the fiber side, because viscose is cellulose and accepts water-based DTG ink much as cotton does. The tradeoffs are the usual ones: DTG shines for photographic or many-color art and for one-off and small orders, but the print sits softer and generally fades sooner than screen print, and dark garments need a pretreat and a heat-cure step you must keep brief and shielded so the platen heat does not glaze the fabric.
Direct-to-film transfers have become the flexible workhorse for tricky fabrics because they apply at a lower temperature than most cotton settings. Practical viscose press guidance runs about 280 to 300°F for 10 to 15 seconds at medium pressure, with a 3 to 5 second pre-press to drive off moisture and a Teflon or parchment sheet over the transfer. If the fabric picks up an unwanted sheen, drop the temperature 10 to 20°F and shorten the dwell. DTF gives you full color with no screens, holds up well when applied correctly, and lands in a sweet spot for short-to-medium runs, though the print is a film sitting on the surface rather than in the cloth, so hand feel is firmer than a good water-based print.
Embroidery, and the method that simply will not work
Sublimation is off the table for true bamboo viscose. Dye sublimation bonds only to polyester, so on a cellulosic bamboo shirt the gas-phase dye has nothing to bind to and the image washes out. If someone quotes you all-over sublimation on a 100% bamboo tee, that is a red flag worth questioning. Embroidery, by contrast, works on any fiber, but lightweight bamboo jersey is thin and drapey, so it puckers easily. It needs a cutaway backing, a slightly looser stitch density, and it is far happier on heavier bamboo pieces such as polos, French terry or caps than on a featherweight 150 gsm tee. Embroidery reads as premium and is effectively permanent, but it adds bulk and is priced by stitch count, so it fits logos rather than large or detailed art.
Matching the method to your order
Once the fabric constraints are handled, the decision usually comes down to color count and quantity. For one or two ink colors at higher volume, screen printing wins on both durability and unit cost. For full-color art, tiny runs, or frequent design changes, DTF or DTG avoids screen setup entirely. The economics are the clearest way to see the crossover: screen printing carries a one-time setup that gets cheaper per shirt as the run grows, while DTF and DTG stay close to a flat rate no matter how many you order.
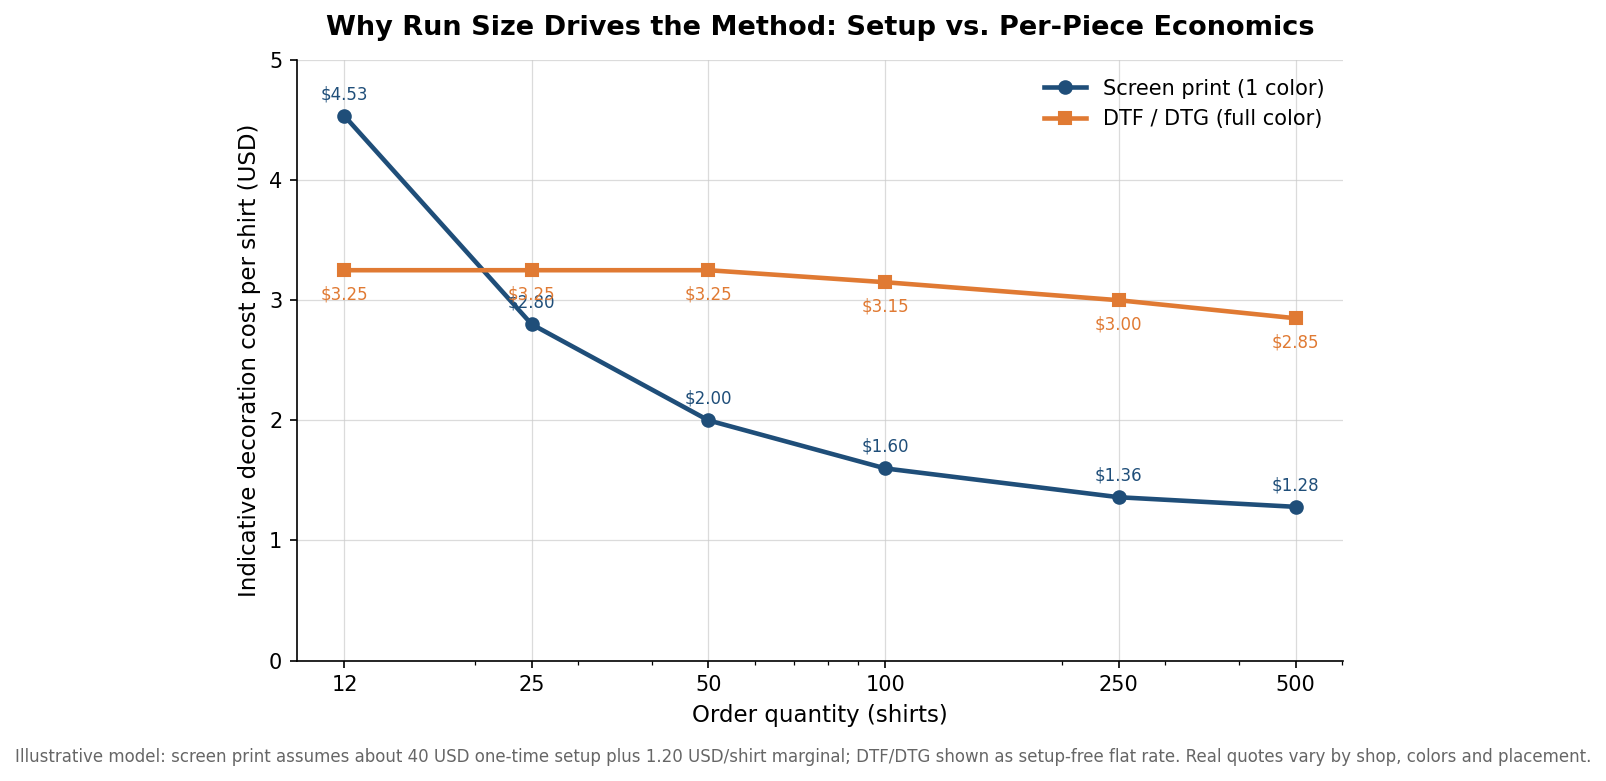
The indicative model above shows why a 12-piece order of a simple logo often prints more cheaply by DTF, while the same logo at 100 or 250 pieces is markedly cheaper by screen. Treat the exact dollar figures as illustrative; real quotes swing with color count, print size, garment cost and shop. The durable takeaways are structural. Confirm your shirt is bamboo viscose and specify a low-temperature process. For volume one-to-three color work, ask for low-cure plastisol and, on colored blanks, a low-bleed ink. For full color or short runs, DTF at roughly 290°F with a protective sheet is the safe default, and DTG is the softer option when hand feel matters most. Reserve embroidery for heavier pieces and logo-scale marks. Get a pressed and washed sample before committing to a production run, because on a fiber this heat-sensitive, a five-minute test wash is the cheapest insurance you can buy.